- Titanium Anode Electrolyzer Manufacturer & Water Electrolysis Hydrogen Solutions Supplier
 拷贝22_xt_seo5050.jpg)
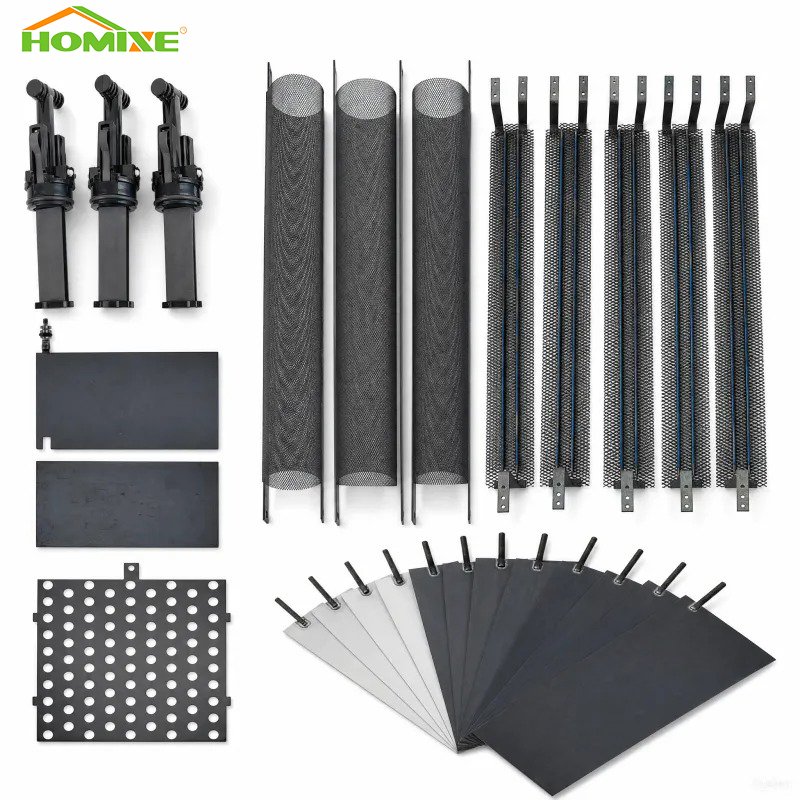
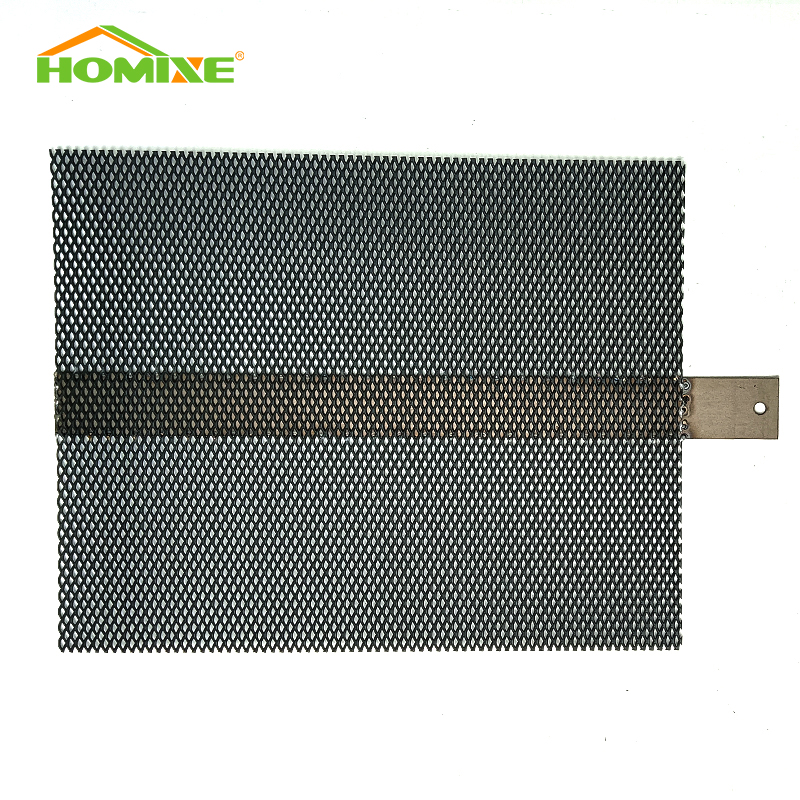
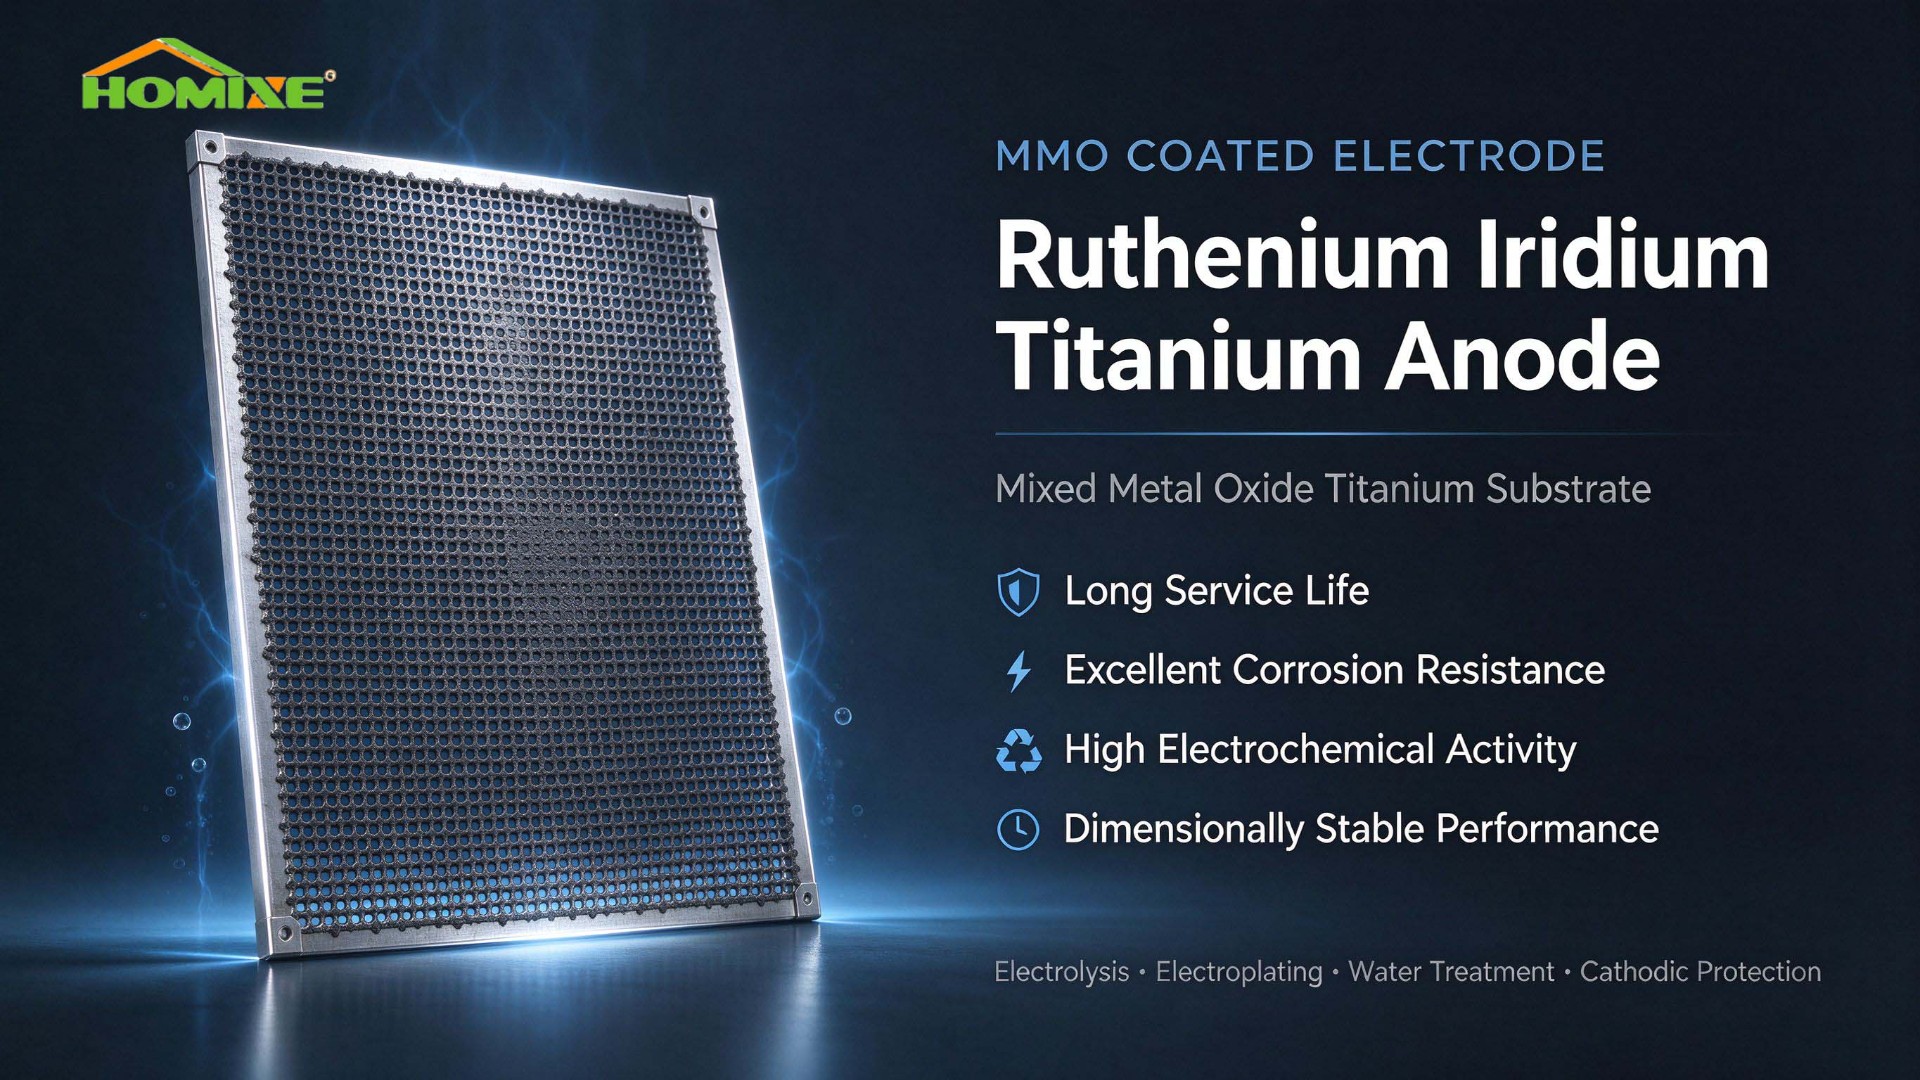
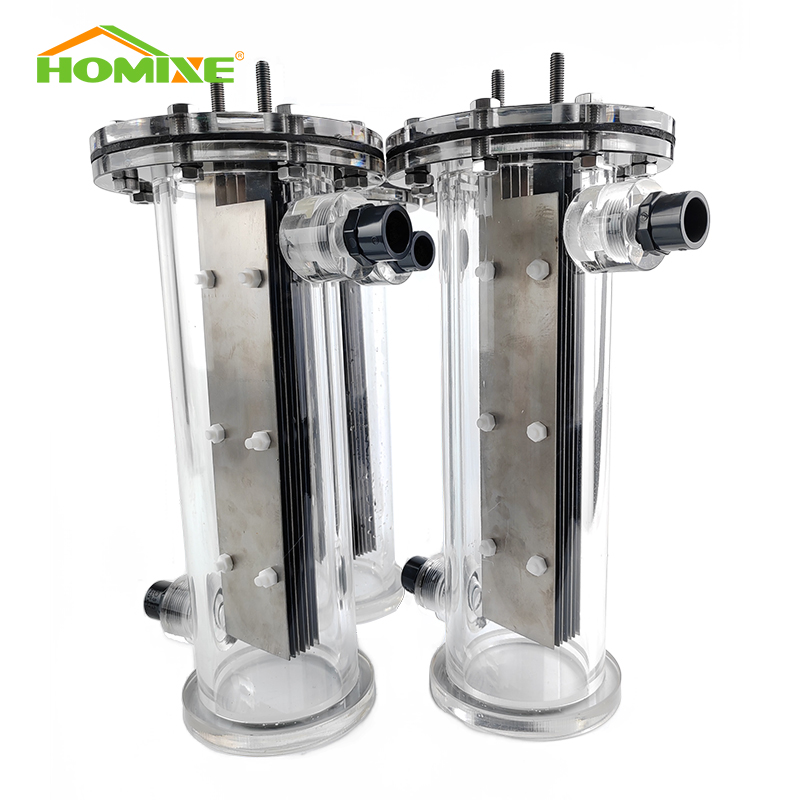
| Product Name | Ruthenium Iridium Titanium Anode (RuO₂-IrO₂ / MMO / DSA) | Brand Name | HOMIXE |
| Model Number | HM-RuIr70 | Feature | Insoluble anode with excellent dimensional stability — electrode spacing and cell voltage stay constant over the whole service life. Low chlorine / oxygen overpotential for lower power consumption (10–30% less DC energy than graphite or lead anodes). High corrosion resistance, long service life, and no metal ion release into the treated water or electrolyte. Recyclable — the titanium substrate can be reused. |
| Grade | GR1 Titanium | Technique | Rolling, Cutting, Welding, Surface Pre-treatment, Thermal Decomposition Coating (RuO₂-IrO₂) |
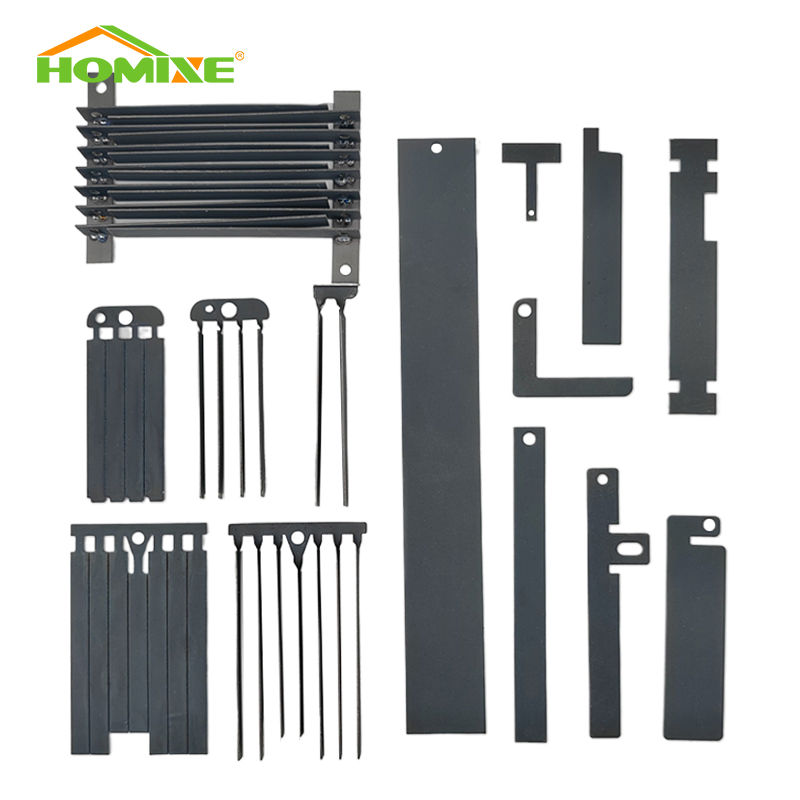
| Application | Water electrolysis & hydrogen generation, on-site sodium hypochlorite generation from brine or seawater, swimming pool, cooling water and aquaculture disinfection, acid electroplating (hard chrome, acid copper, nickel), PCB and copper foil plating, wastewater electro-oxidation, electrowinning & metal recovery, impressed current cathodic protection (ICCP), electrolytic water treatment. | Dimension | Customized size — plate / mesh / rod / tube, made to drawing |
| Coating | Ruthenium Iridium (RuO₂-IrO₂) | Coating Thickness | 8–20 g/m² precious metal loading (Ru + Ir) |
An Ru-Ir anode is one of two MMO coatings on a titanium substrate. It is the coating of choice when the cell produces chlorine or hypochlorite — the half of MMO chemistry built for low-voltage, long-life chlorine evolution.
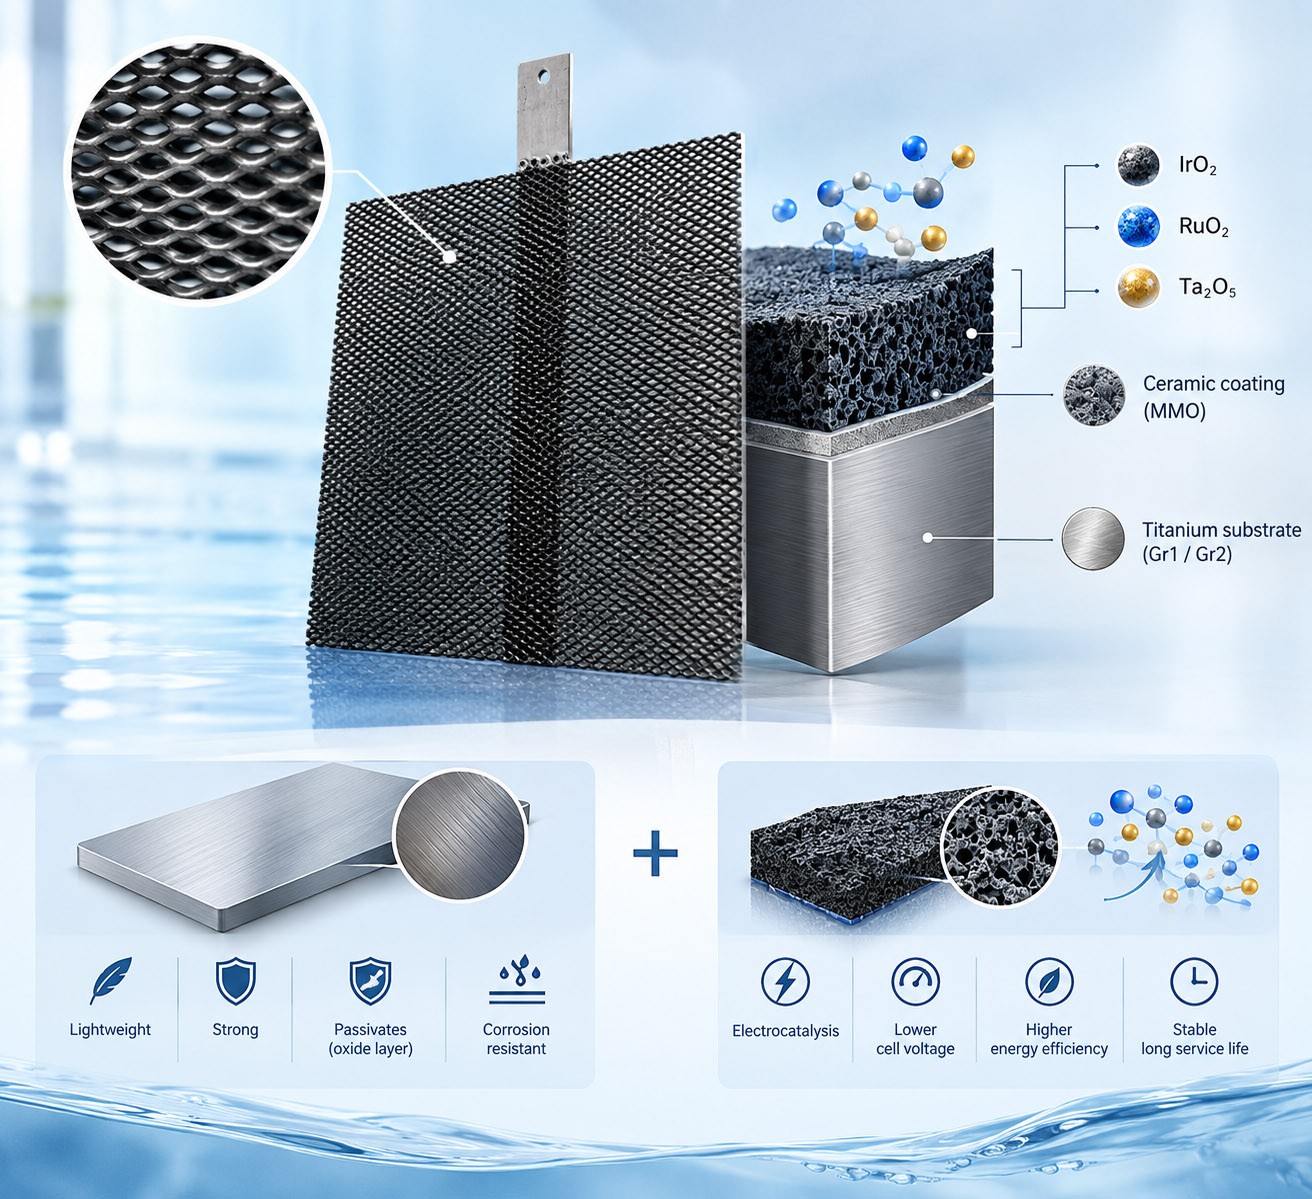
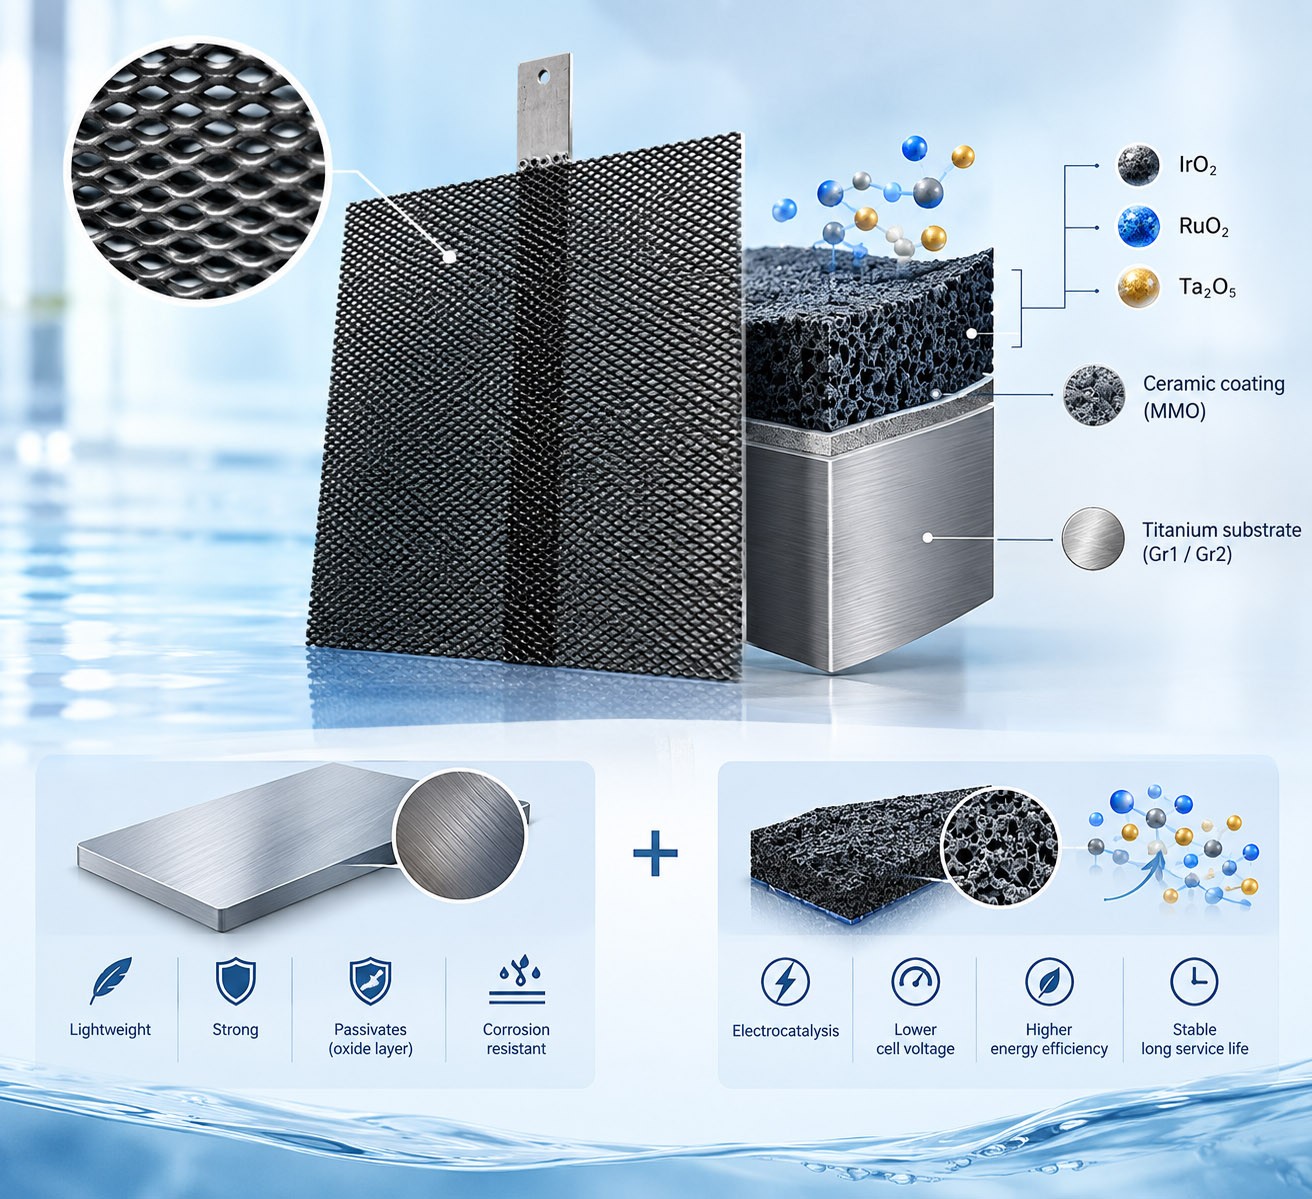
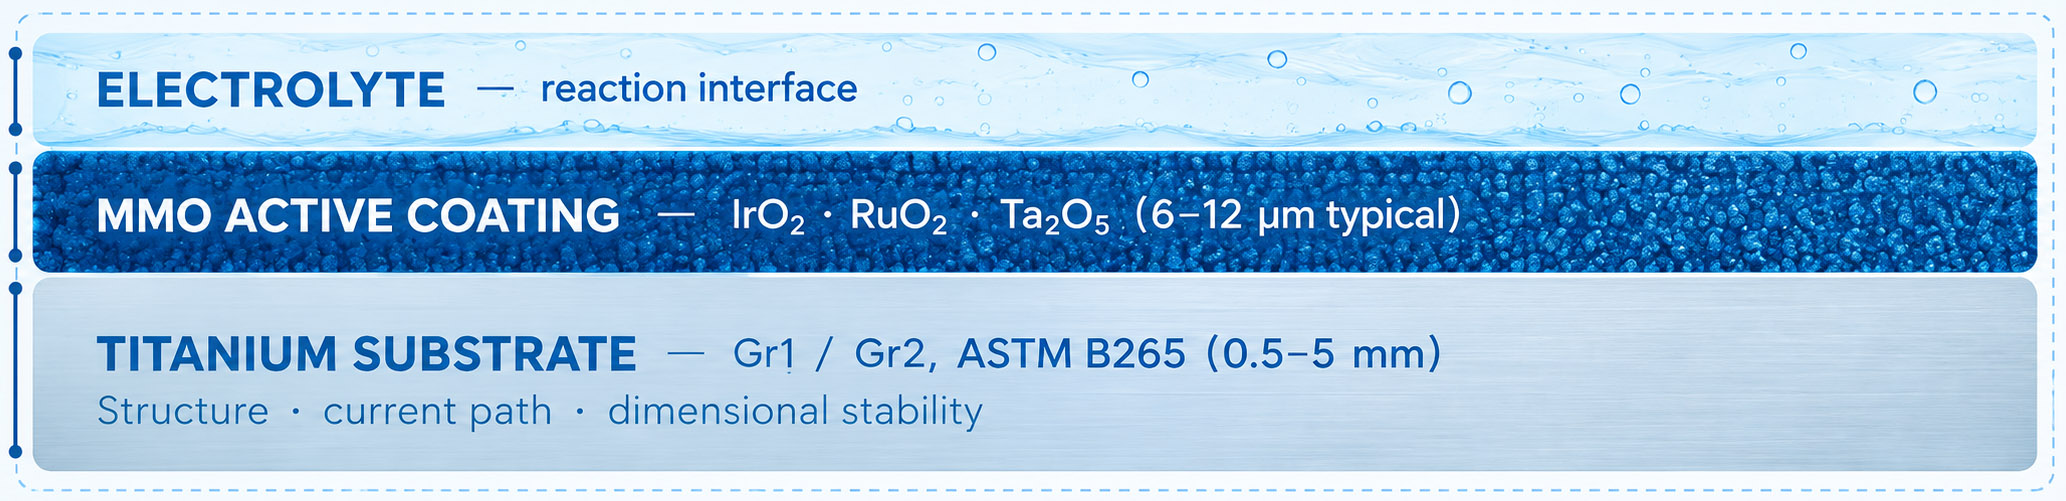
A ruthenium-iridium titanium anode is part of the MMO (mixed metal oxide) family, also known as DSA — dimensionally stable anode. A commercially pure titanium substrate (Gr1 or Gr2) carries a thin ceramic coating of ruthenium oxide (RuO₂) and iridium oxide (IrO₂), applied by thermal decomposition and sintered at high temperature until it fuses to the titanium surface.
The two oxides do different jobs. Ruthenium provides the chlorine-evolution catalysis — it has the lowest chlorine overpotential of the MMO family, so more of the supplied current converts to Cl₂ instead of wasted O₂. Iridium stabilises the ruthenium, slows coating loss and extends service life. The titanium substrate provides the structure and current path: light, strong, and once anodised, it forms a passive oxide skin that resists attack instead of dissolving.
That combination is what sits behind the savings. Lower cell voltage means fewer kWh per kilogram of hypochlorite produced or per cubic metre of water chlorinated. Because the titanium is virtually insoluble, the electrode gap stays fixed for the service life — the cell voltage does not drift, and the coating does not contaminate the electrolyte.
Graphite erodes and widens the electrode gap; lead anodes deform, short out and put lead ions into the water. Ru-Ir anodes hold their geometry, run at 10–30% lower DC energy consumption, and the titanium substrate can be re-coated instead of scrapped.
Reference ranges for coated titanium electrodes. Actual performance depends on electrolyte, current density, temperature and duty cycle.
| Property | Graphite | Lead alloy | MMO / Ti |
| Dimensional stability | Poor — erodes | Moderate — deforms | Excellent — no shape change |
| Overpotential | High | High | Low |
| DC energy saving | Baseline | Baseline | 10–30% lower |
| Product contamination | Carbon particles | Lead dissolution | Negligible |
| Typical service life | 3–12 months | 1–3 years | 1–8+ years, recoatable |
Answer these four and the electrode specifies itself. If you only know the application, send that — our engineers will work through the rest with you.
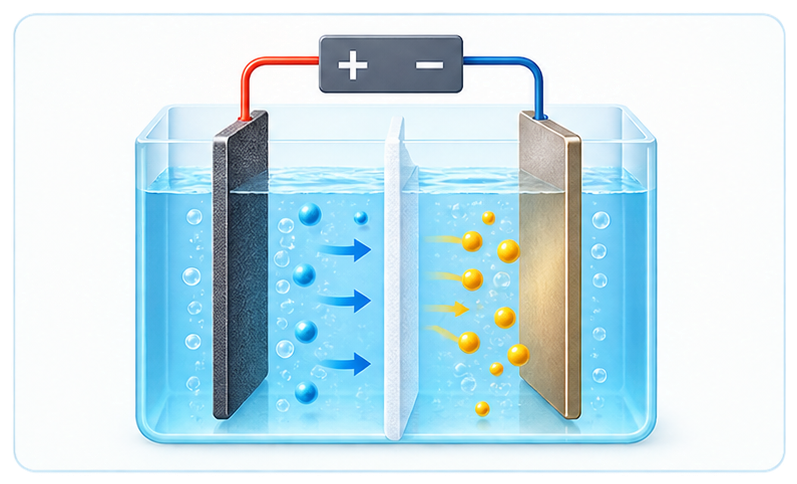
If yes — brine, seawater, salt pool, chlor-alkali, on-site hypochlorite — you are in the Ru-Ir zone. Chlorine evolution (CER) is what ruthenium oxide is for. If the cell is producing oxygen (acid plating, electrowinning, copper foil, water electrolysis), see our Ir-Ta page instead. Getting this one wrong is the most expensive mistake in anode selection — the wrong family can fail within weeks.
Send us the composition, pH, operating temperature and chloride level. Acidic sulfate or nitrate media point to Ir-Ta. Brine, seawater and hypochlorite duty point to Ru-Ir. Fluoride above roughly 20 ppm needs review before anything is specified — it attacks both the titanium and most oxide coatings.
Give us the design current density (A/m²), the maximum you will ever push, and the active area. Current density is the main lever on coating load and therefore on service life. Ru-Ir is the most chloride-sensitive MMO coating to deliberate polarity reversal — tell us if the controller ever swaps polarity, because that drives the answer toward platinized titanium.
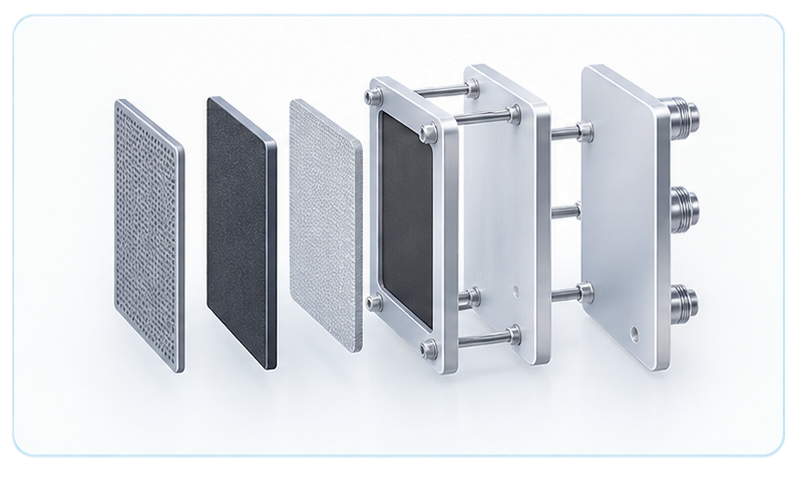
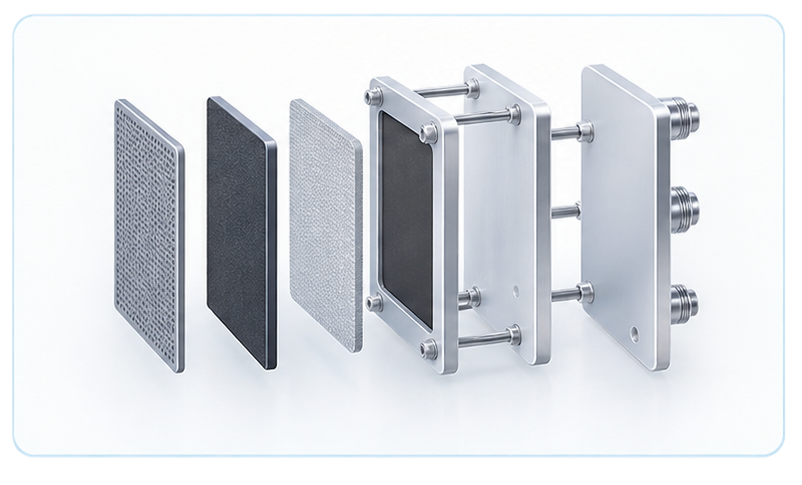
Plate, expanded mesh, perforated plate, rod, tube, ribbon, wire or disc — plus how the anode connects: tab, bolt hole, thread, weld lug, busbar, cable or your own design. Send a drawing if you have one. No drawing? A photo with dimensions is enough for us to draft it for your approval.
Ir-Ta MMO is the right call when
| VS | Ru-Ir MMO is the right call when
|
| Two constraints apply to every MMO anode: avoid deliberate polarity reversal (the oxide coating is not designed for it — choose platinized titanium if your controller reverses), and keep the anode inside its rated temperature and fluoride limits. Send us your process data and we will tell you honestly whether MMO belongs in your cell. | ||
All three are titanium-based insoluble anodes. Out of the box they look almost identical. Inside the cell they behave very differently — choose by the reaction and the electrolyte, not by price per piece.
Ir-Ta MMO — oxygen evolutionIridium-tantalum oxide (IrO₂-Ta₂O₅) with a low oxygen overpotential and a tantalum-oxide stabiliser that resists acid attack. The standard choice for acid plating, electrowinning, copper foil, PCB plating, electro-oxidation wastewater treatment and industrial water electrolysis. | Ru-Ir MMO — chlorine evolutionRuthenium-iridium oxide (RuO₂-IrO₂). Ruthenium has the lowest chlorine overpotential of the family, so brine cells convert more current into chlorine instead of oxygen. The iridium stabilises the ruthenium and extends coating life. For on-site hypochlorite, pool and cooling-water disinfection and seawater duty. | Pt/Ti — metallic platinumPlatinized titanium carries metallic platinum rather than an oxide — 0.2–20 μm, electro-deposited. It tolerates polarity reversal and intermittent operation far better than any oxide coating, and it cannot contaminate the electrolyte, which is why it is used in precious-metal plating baths and water ionizers. |
| Parameter | MMO — IrO₂-Ta₂O₅ | Ru-Ir — RuO₂-IrO₂★ | Pt/Ti — platinum |
| Primary reaction | Oxygen evolution (OER) | Chlorine evolution (CER) | Both, plus cathodic protection |
| Overpotential | Low for O₂ | Lowest for Cl₂ | Moderate, most stable |
| Coating form | Ceramic oxide, consumed by catalysis | Ceramic oxide, consumed by catalysis | Metallic Pt, dissolves very slowly |
| Typical load | Ir 8–25 g/m² | Ru+Ir 8–20 g/m² | 0.2–20 μm thickness |
| Current density | Highest — up to 2,000–5,000 A/m² | 1,000–3,000 A/m² | Moderate, set by Pt thickness |
| Polarity reversal | Not recommended | Most sensitive — avoid | Tolerated |
| Electrolyte match | Acid / neutral (OER) | Brine / seawater / chloride | Sulfuric acid, plating baths, clean water |
| Contaminates electrolyte? | No | No | No |
| Relative cost per m² | Low–medium | Medium | Highest |
| Relative service life | Long | Long | Long; scales with thickness |
| Recoating | Available, subject to substrate condition | Available, subject to substrate condition | Available, subject to substrate condition |
Numbers: coating load and current-density ranges are typical industry values —
confirm the ranges your own workshop specifies before publishing, and keep the wording identical across every page.
Inconsistent figures on one site are the fastest way to lose an engineer's trust.
Ruthenium-iridium is the MMO coating for chlorine evolution. The first four duties below are built on it. For oxygen-evolution duties the better coating is usually Ir-Ta — but where the electrolyte is chloride-bearing, Ru-Ir is often the practical answer for both reactions.
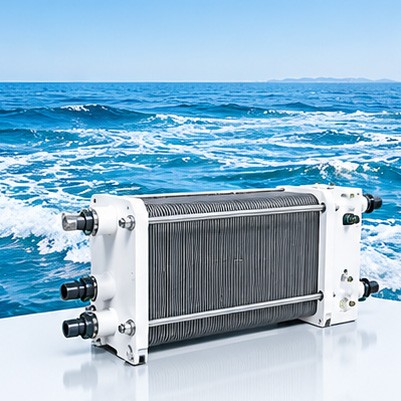
Industrial seawater and brine electrolysis for chlorine or hypochlorite production. Lowest Cl₂ overpotential and stable voltage over thousands of hours are the design drivers.
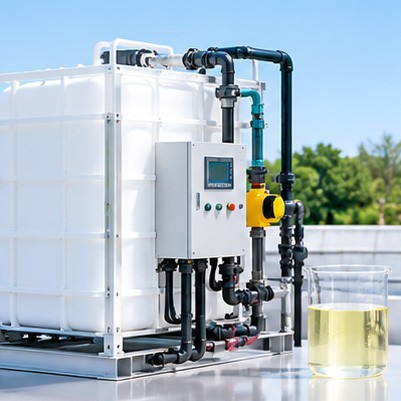
Seawater / brine electrolyzers for on-site NaOCl production. The standard duty for Ru-Ir — water plants, ships, remote sites, gas-field produced water.
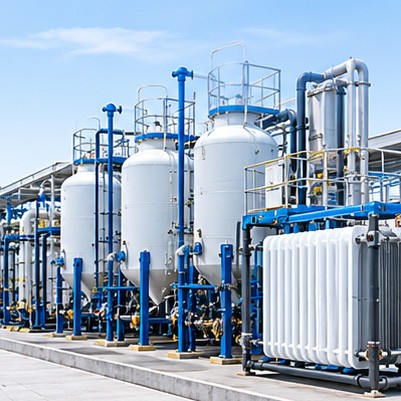
Membrane chlor-alkali cells, chlorate production, HCl electrolysis. High current density, long cell life — the historical home of the Ru-Ir coating.
Salt-water pool chlorination, fish-farm and coastal facility disinfection, sea water electrolysis cells. Chlorine output and cell voltage are the design drivers.
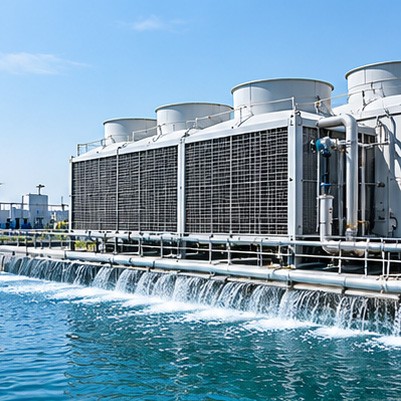
Power-station and industrial cooling-tower biofouling control, marine ballast-water electrochlorination, intake screens. Brackish and seawater duty suit Ru-Ir.
On-site chlorine / hypochlorite generation for water utilities and industrial process water. Same equipment family as the salt-pool cell, sized for throughput.
For effluents with chloride, Ru-Ir is often the practical choice because the electrolyte would attack Ir-Ta. For chloride-free waters, Ir-Ta is the better answer.
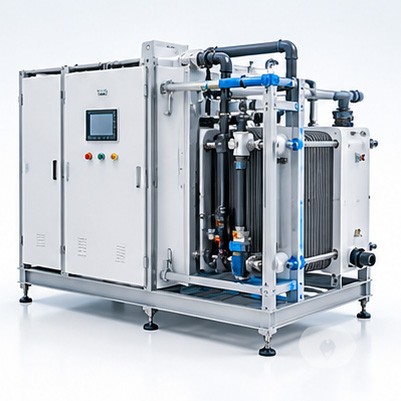
Electrolyzer builders, disinfection-equipment makers and water-treatment OEMs who need a repeatable electrode built to a controlled drawing, batch after batch.
Geometry and coating have to be designed together — the shape decides the active area and the current distribution, the coating decides the reaction. Tell us the cell, and we build the shape that fits it.
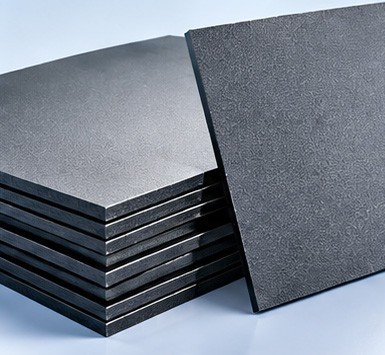
Flat plate, perforated plate and profiled sheet. Defined active area, tab or busbar connection. The workhorse form for electrolysis cells and electroplating.
Thickness 0.5–5 mm · up to 1,000 mm
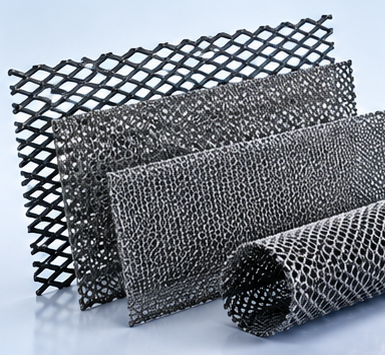
Woven mesh, expanded mesh and knitted mesh. High active surface per unit weight, low flow resistance — the standard for water treatment, pool cells and ionizers.
Mesh sizes to drawing
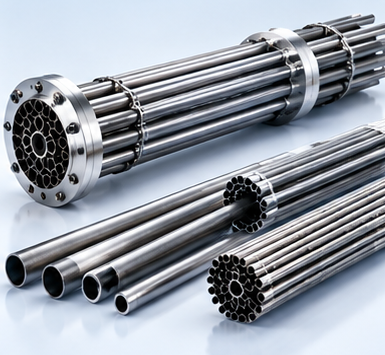
Tubular anodes with active length masked to spec, threaded, welded or cable-ended. Used in impressed-current cathodic protection, deep-well beds and compact cells.
Ø, active length, mounting to drawing
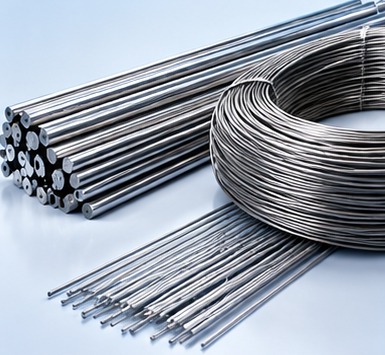
Solid rod and wire anodes with defined active zones, threaded ends or welded connections. For compact reactors, plating jigs and internal cell duties.
Ø to drawing · active zone masked
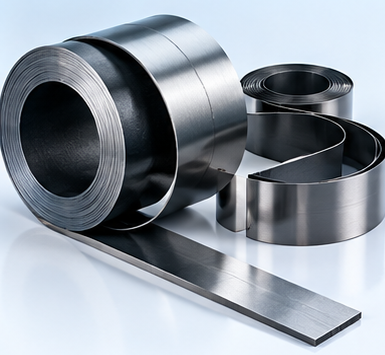
Thin flexible ribbon for tank-bottom, vessel and pipeline protection where the surface is irregular. Coated zone defined to your layout.
Width / thickness to drawing
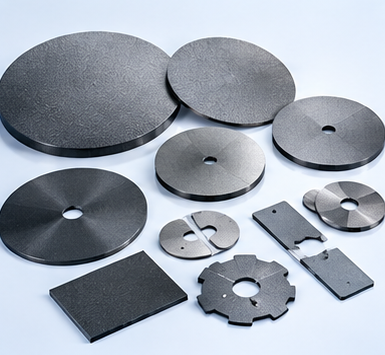
Disc, cone, spiral and 3D shapes for compact electrolysis cells where installation space or flow pattern dictates the form factor.
Build to drawing
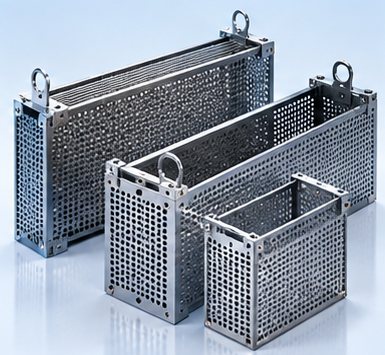
Titanium baskets that hold nickel, copper or precious-metal anode balls in plating and metal-recovery lines. Separate category — not a coated active anode.
Perforated / mesh / custom
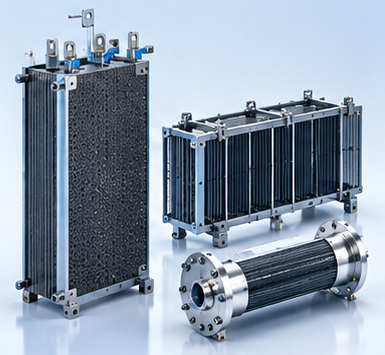
Not on the list? That is the normal case. Most of what we ship is a geometry that existed only on the customer's drawing a week earlier.
PDF · DWG · STEP · IGES · STL
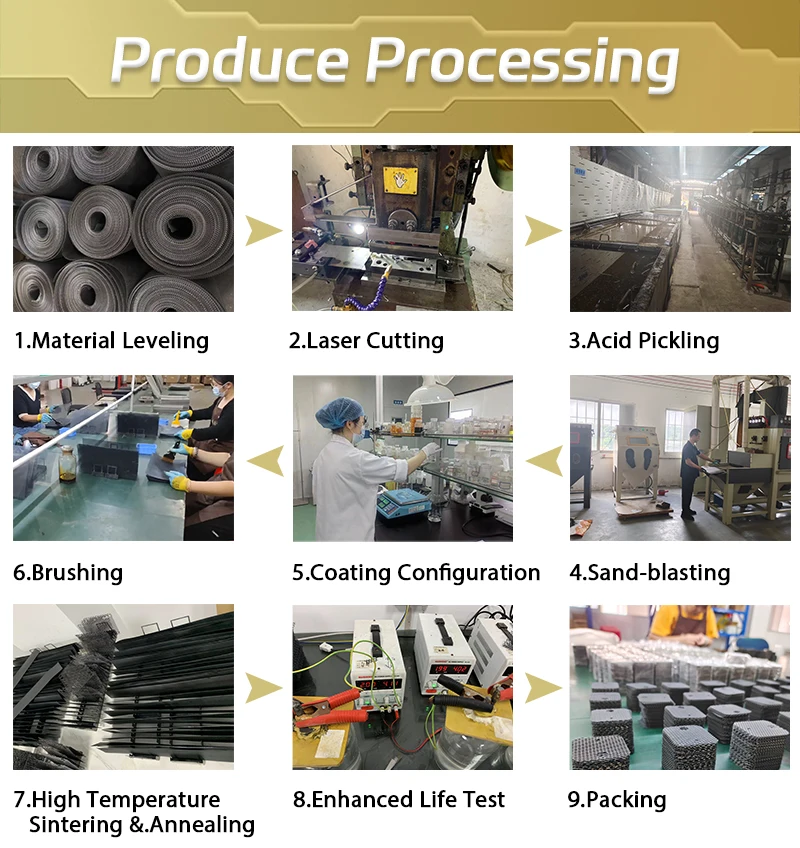
Every HOMIXE MMO anode is produced and inspected in-house, batch by batch. You receive the electrode — and the records behind it.
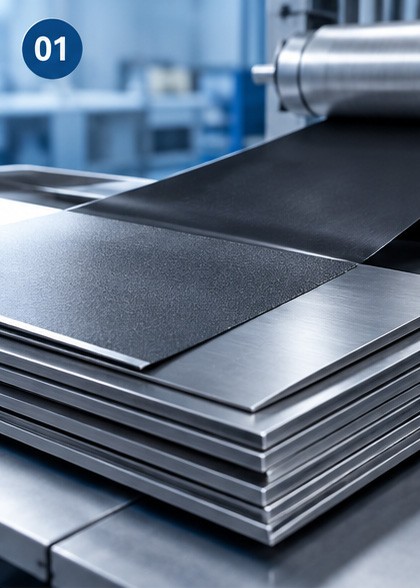
Incoming Gr1 / Gr2 titanium verified against ASTM B265 by material certificate and composition check. Grade and heat number recorded before release to production.
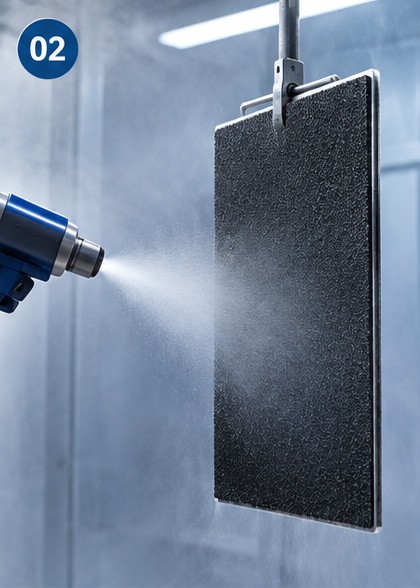
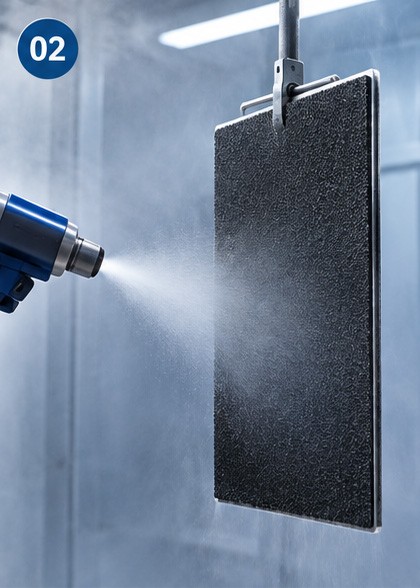
Sand blasting and acid etching remove oxide scale and create the anchor profile the Ru-Ir coating needs in order to bond. An under-prepared surface is the single most common cause of premature coating loss.
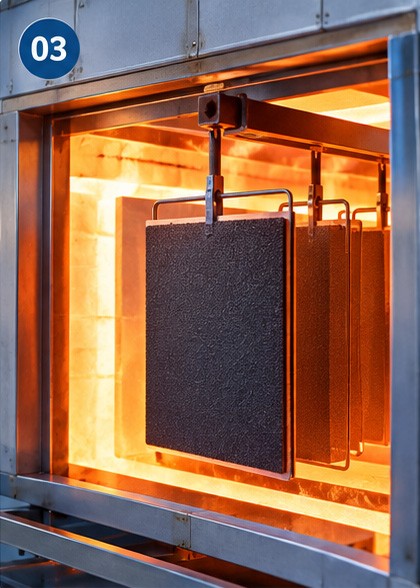
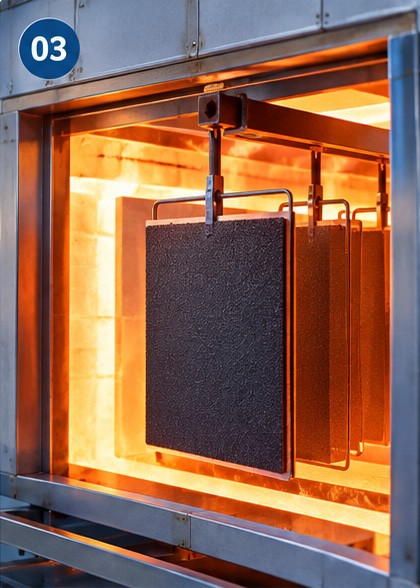
Precursor salts applied in multiple controlled passes and sintered at 400–450 °C. Coating load is set to your specification and confirmed by weight gain.
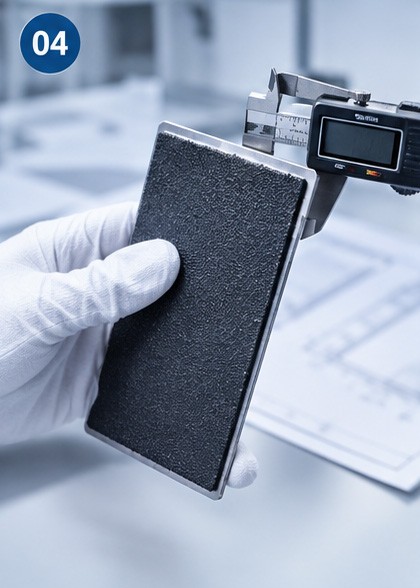
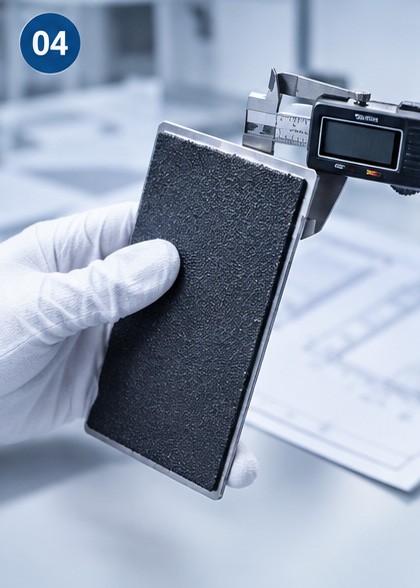
Dimensions, active/coated zones, masking, tab, thread or lug, flatness and edge condition checked against the approved drawing.
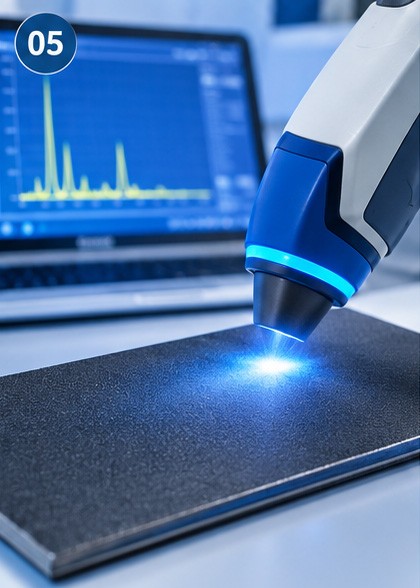
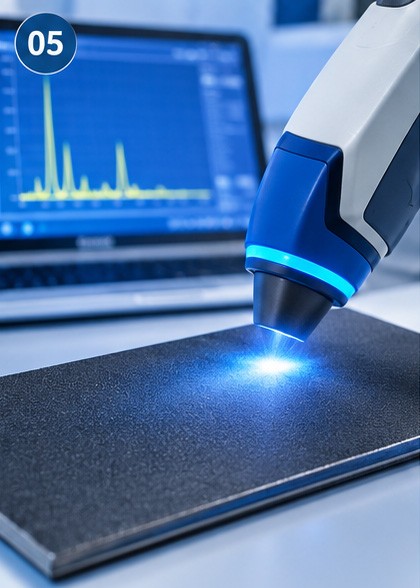
Coating thickness and surface examined; XRF measurement recorded for the batch. Adhesion checked on production samples.
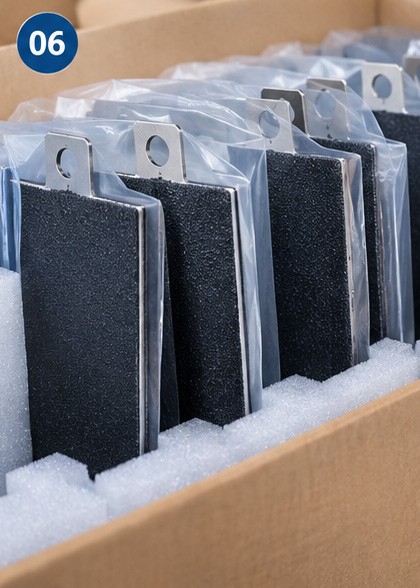
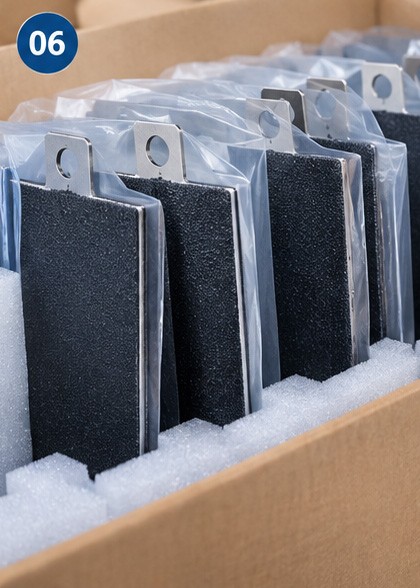
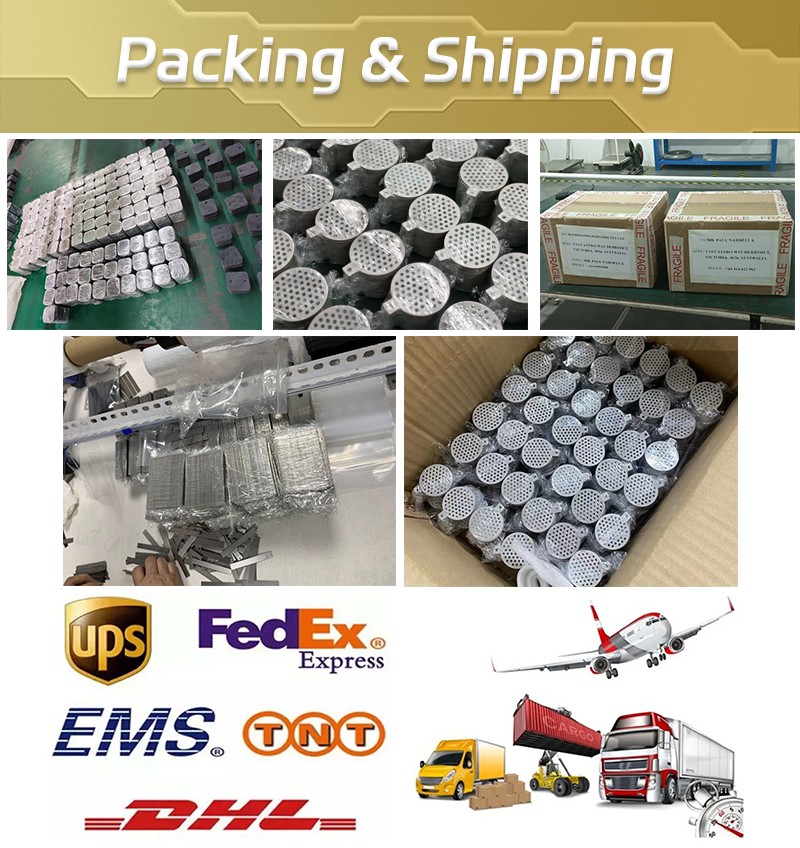
Appearance, identity marking and packing checked. Electrodes protected individually for export so the coating arrives with no transit damage.
Two anodes that look identical can differ threefold in price. These are the six reasons — so you can compare quotations on the same basis instead of on the headline number.
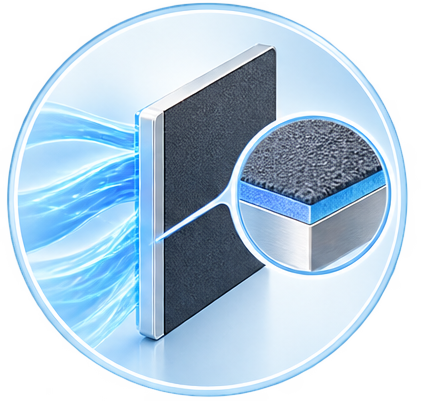
The single largest driver. Precious-metal loading is quoted per m², so a 25 g/m² Ir-Ta anode contains several times the iridium of an 8 g/m² anode — and lasts correspondingly longer. Under-specifying load is a false economy.
You pay for the coated area, not the blank size. Masking, defined active windows and edge treatment all add process steps but prevent wasted coating.
Plate is cheapest. Expanded mesh, woven mesh, tube, machined discs and welded assemblies each add cutting, forming and welding operations.
A plain tab costs nothing. A machined thread, a copper-titanium clad bar or a cable with a sealing gland is real engineering, and it is also what stops a joint from overheating later.
Turned dimensions, XRF reports, adhesion tests, MTC and batch traceability all take time. If a project needs a full documentation pack, say so up front so it is priced in rather than added later.
Setup dominates small orders; unit price falls with volume. A repeat order against a held drawing is the cheapest electrode you will ever buy.
A factory-direct manufacturer of electrocatalytic titanium electrodes — built to your drawing, your cell and your duty cycle.
Because we make the electrode ourselves — we do not simply resell it. HOMIXE has focused on electrocatalytic titanium electrodes since 2013, producing MMO anodes, ruthenium-iridium anodes and platinized anodes in our own workshop in Foshan, China.
Buying factory-direct means no middleman markup, engineering support on your specification before production starts, and direct control over coating load, adhesion and batch quality. Every order ships traceable to its own inspection records — from a 5-piece sample to OEM production volumes.
We manufacture all three coating families, so our recommendation is based on your duty cycle rather than on whatever is sitting in stock. Send us your electrolyte, current density and running hours, and we will tell you honestly which coating belongs in your cell.
OEM & Customized Solutions
Different projects require different electrode dimensions, coating systems, cell structures and electrical configurations. HOMIXE supports customized solutions for OEM manufacturers, water treatment companies and system integrators.


 EN